Products Knowledge
Why Vietnam Is a Leading Destination for Beverage Manufacturing
Sep
Beverage Manufacturing in Vietnam covers a broad range of product categories, including fruit juice drinks, coconut water, aloe vera beverages, concentrated juices, ready-to-drink coffee, and customized private label products. For international companies, sourcing beverages from Vietnam can provide access to customized formulations, different packaging formats, scalable production, and export-oriented manufacturing services. More importantly, modern Vietnamese beverage factories are increasingly capable of supporting the complete product development cycle, from concept and formula development to commercial production, quality control, packaging, and shipment preparation. This makes Vietnam a practical manufacturing destination for brands seeking to develop differentiated beverage products for international markets.
1. Why Vietnam Has Become an Attractive Beverage Manufacturing Hub
Vietnam’s position in the beverage industry is supported by several interconnected factors. The country has a developed agricultural supply chain, a growing food-processing sector, a strategic location in Asia, and an increasingly export-oriented manufacturing ecosystem.
Strong Agricultural Resources
Vietnam is known for producing a wide range of tropical and subtropical fruits. Mango, pineapple, passion fruit, coconut, orange, guava, dragon fruit, soursop, and other agricultural products can provide important raw materials for beverage production.
For beverage companies, access to diverse fruit ingredients creates opportunities to develop products with distinctive flavor profiles. Tropical fruit beverages can be positioned for consumers who are interested in refreshing, convenient, and fruit-based drinks.
The availability of local agricultural resources can also support product diversification. A manufacturer may develop several flavors using related ingredients, allowing brands to build a broader product portfolio without completely changing their manufacturing strategy.
Established Food-Processing Capabilities
Vietnam’s food-processing industry has developed significantly over the years. Modern processing facilities increasingly use controlled production systems designed to support consistent quality and commercial-scale manufacturing.
This development has created opportunities for international companies that require more than basic contract filling. Beverage manufacturers can provide services covering product development, ingredient processing, blending, filling, packaging, quality control, and export preparation.
Strategic Location in Asia
Vietnam’s geographical position provides access to major Asian markets and international trade routes. This is relevant for beverage companies managing supply chains across Asia, the Middle East, Europe, Africa, and other regions.
A strategic manufacturing location can help businesses coordinate raw materials, production, warehousing, and international transportation more efficiently.
2. Beverage Manufacturing in Vietnam: From Concept to Finished Product
Modern beverage production involves considerably more than filling a liquid into a container. International brands often require a complete development process that connects product formulation, manufacturing, packaging, and quality management.
Product Concept Development
The manufacturing process typically begins with a product concept. Buyers may provide information about their target consumers, preferred flavors, packaging sizes, price positioning, and destination market.
The manufacturer can then evaluate the concept and determine the appropriate production approach. For example, a brand looking to introduce a tropical fruit beverage may require a specific combination of fruit ingredients, sweetness, acidity, and flavor intensity.
A clearly defined product concept helps create a more efficient development process because technical and commercial requirements can be considered from the beginning.
Formula Development and Sampling
Formula development is an important stage in customized beverage production. Manufacturers may adjust ingredients and technical parameters to achieve the desired taste, appearance, and product characteristics.
Samples allow buyers to evaluate the proposed formulation before moving to commercial production. If necessary, the formula can be adjusted through additional sampling rounds.
This process is particularly valuable for private label and OEM projects because the final product must reflect the brand’s requirements rather than simply follow a standardized factory formula.
Commercial-Scale Production
After the formula, packaging, and specifications have been approved, production can move to the commercial stage.
Large-scale production requires controlled ingredient handling, accurate processing, consistent filling, and systematic quality inspection. Production procedures should be designed to maintain consistency between batches and ensure that finished products meet the approved specifications.
3. The Role of Technology in Vietnamese Beverage Manufacturing
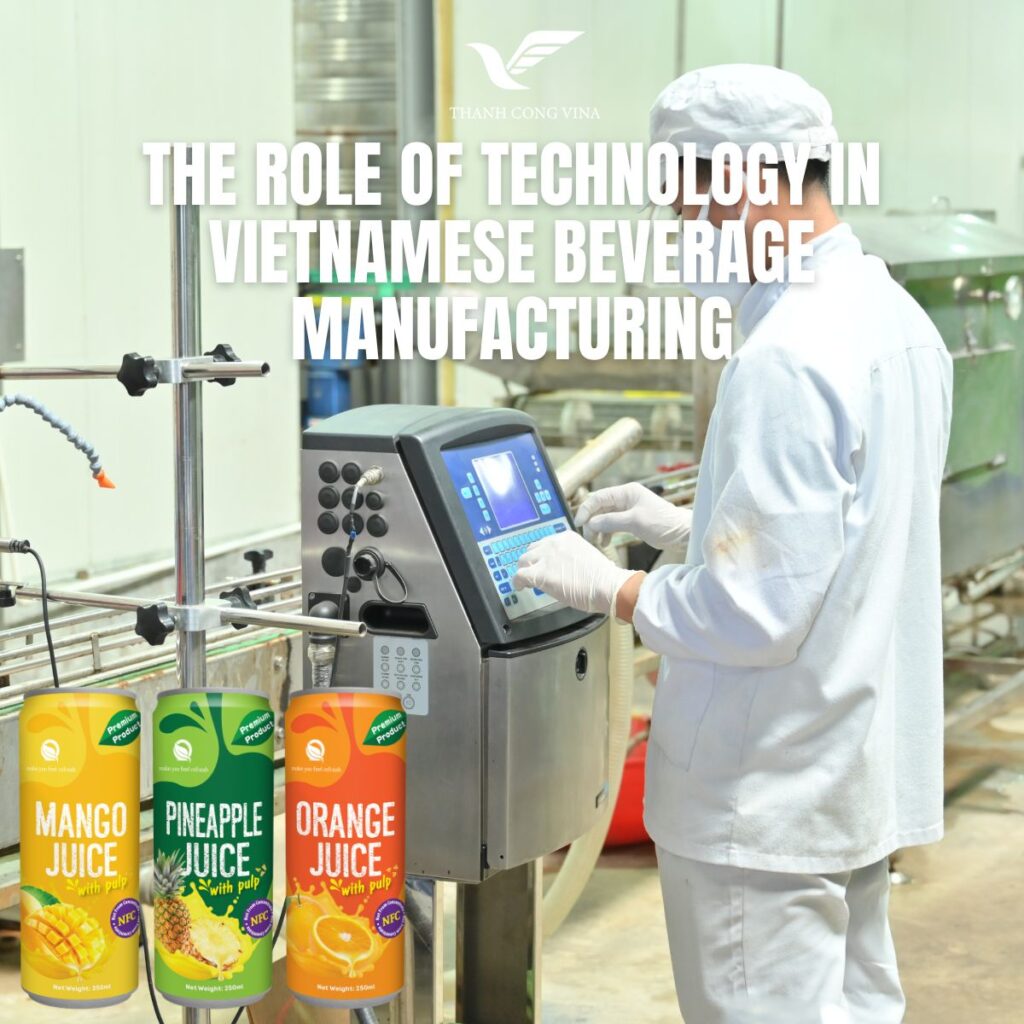
Technology plays an increasingly important role in improving production efficiency, product consistency, and quality management.
Modern Processing Systems
Beverage factories use different processing technologies depending on the characteristics of the product. Juice drinks, coconut water, aloe vera beverages, concentrated juices, and ready-to-drink coffee may require different processing and filling approaches.
Controlled processing helps manufacturers maintain consistent product characteristics across commercial batches. The specific production process is selected according to the formula, packaging format, product specifications, and market requirements.
Automated Filling and Packaging
Filling accuracy is essential for commercial beverage production. Modern equipment can support consistent filling volumes while improving production efficiency.
Packaging operations may include filling, sealing, coding, labeling, carton packing, and pallet preparation. Coordinating these stages within an organized production system can reduce handling errors and support consistent finished products.
Production Traceability
Traceability is another important element of modern beverage production. Manufacturing records can help identify raw materials, production batches, packaging information, and quality-control activities.
For international buyers, traceability provides useful information for supply-chain management and quality assurance. It also supports communication between manufacturers, distributors, importers, and retailers.
4. Product Diversity and Customization Opportunities
One reason international businesses consider Vietnam is the flexibility available for developing different beverage concepts.
Fruit Juice Drinks
Fruit juice drinks represent one of the most versatile categories in the beverage market. Manufacturers can develop products using different fruit flavors and combinations according to the requirements of individual brands.
Popular concepts may include mango, orange, pineapple, passion fruit, guava, peach, soursop, and other fruit-based beverages.
Customization can involve flavor profiles, fruit content, sweetness, acidity, packaging size, and visual presentation.
Coconut-Based Beverages
Vietnam’s strong coconut-growing sector provides opportunities for coconut-based beverage development.
Coconut water can be marketed as a refreshing beverage and may also be combined with fruit flavors to create differentiated product concepts. Coconut water mixed with mango, strawberry, calamansi, or other fruit flavors can provide additional opportunities for brands looking to expand their beverage portfolio.
Aloe Vera and Functional-Style Beverages
Aloe vera drinks are another category that can be developed for different international markets. Aloe vera pieces can provide a distinctive drinking experience while allowing brands to create visually differentiated products.
Depending on the target market, manufacturers can develop different flavor combinations and packaging formats.
Ready-to-Drink Coffee
Vietnam also has a strong coffee culture and established coffee-processing industry. This creates opportunities for ready-to-drink coffee products such as black coffee, milk coffee, latte, or cappuccino.
RTD coffee can be developed in convenient formats suitable for supermarkets, convenience stores, food-service channels, and other retail environments.
5. Quality and Food Safety in Beverage Manufacturing
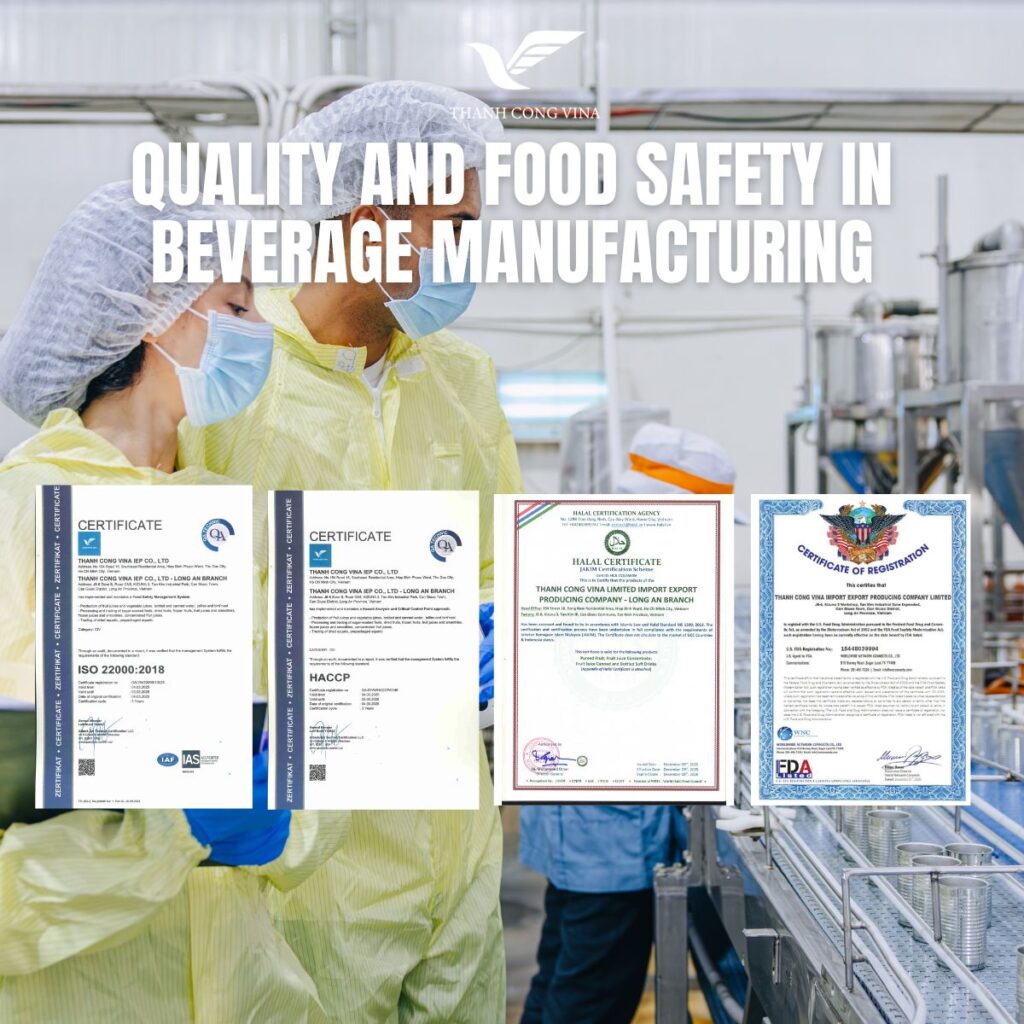
Quality management is a critical consideration for international beverage buyers. Product consistency, food safety, raw material control, and finished-product inspection all contribute to a successful supply chain.
Raw Material Quality Control
The quality of the finished beverage begins with its ingredients. Raw materials should be assessed according to applicable specifications before entering production.
Ingredient control may involve documentation review, visual inspection, specifications, storage conditions, and other relevant checks.
For fruit-based beverages, consistent raw material quality is particularly important because changes in ingredients can affect flavor, color, aroma, and overall product characteristics.
Manufacturing Process Control
Production parameters must be managed according to the approved product specifications. Controlled processing helps reduce variations between batches.
Quality teams can monitor relevant production stages to ensure that the beverage is processed and packaged according to established procedures.
Finished Product Inspection
Before shipment, finished products can be inspected according to the agreed specifications. Quality checks may cover appearance, taste, packaging integrity, coding, quantity, and other product requirements.
For export products, documentation and traceability are also important components of quality management.
6. Custom Packaging and Private Label Manufacturing
Packaging has become an essential component of beverage branding. For international companies, customized packaging can help create a recognizable identity while adapting the product to specific retail channels.
Flexible Packaging Formats
Different beverage categories can use different packaging formats depending on product requirements and target markets.
Common commercial formats include cans, PET bottles, glass bottles, and other suitable containers. Product sizes may also vary, with options such as 250ml, 330ml, 500ml, and other customized specifications.
The appropriate format depends on the product, distribution channel, consumer preferences, transportation requirements, and brand positioning.
Customized Brand Design
Private label production allows companies to manufacture beverages under their own brand names. Manufacturers can coordinate with buyers on labels, artwork, product information, packaging specifications, and carton design.
A successful packaging project requires technical coordination because artwork must correspond with the actual container dimensions and manufacturing requirements.
Packaging for International Distribution
Export packaging should provide sufficient protection throughout transportation and storage. Carton configuration, palletization, product weight, and container loading should be considered during production planning.
Efficient packaging can also contribute to better logistics management by making more effective use of available container space.
7. Export Advantages of Beverage Manufacturing in Vietnam
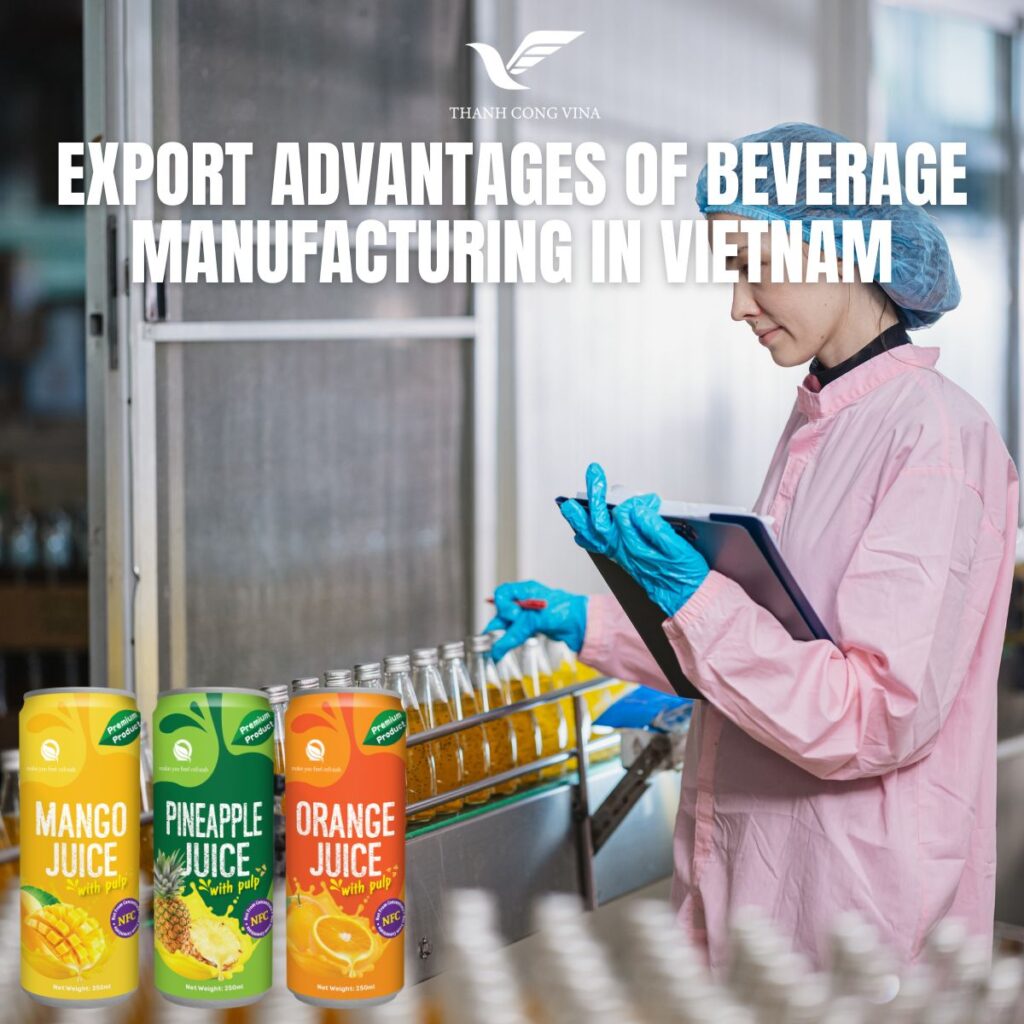
Vietnam’s beverage industry is increasingly connected to international supply chains. For global buyers, export-oriented manufacturing requires coordination across production, documentation, logistics, and destination-market requirements.
International Market Requirements
Every destination market can have its own requirements related to ingredients, labeling, packaging, food safety, and documentation.
Manufacturers working with international buyers need to understand the specifications provided by the customer and coordinate production accordingly.
This may include customized labels, ingredient declarations, nutrition information, product specifications, certificates, and other documentation requested for a particular market.
Export Documentation and Shipment Preparation
Export orders require careful preparation before products leave the factory. Depending on the destination and commercial arrangement, buyers may require production information and shipment-related documentation.
The manufacturing team can coordinate with buyers and logistics partners to prepare the necessary information for international shipment.
Support for Global Distribution
An export-oriented beverage manufacturer should understand the requirements of different supply-chain participants. Products may move from the factory to importers, distributors, supermarkets, convenience stores, restaurants, hotels, or other commercial channels.
Coordinated production and shipment planning can help international buyers manage their beverage supply more effectively.
8. How to Select the Right Beverage Manufacturing Partner in Vietnam
Choosing a suitable manufacturing partner is an important decision for brands planning to launch or expand a beverage portfolio.
Evaluate Manufacturing Capabilities
Buyers should first assess whether the factory can manufacture the required product category. Relevant capabilities may include fruit juice production, coconut water processing, aloe vera beverages, concentrated juice, RTD coffee, and customized beverage development.
The ability to handle multiple product categories can provide greater flexibility when brands expand their portfolios.
Review Customization Services
A manufacturing partner should be able to discuss product concepts, formulation, packaging, MOQ, production planning, and other commercial requirements.
For private label projects, customization capability is particularly important because the final product needs to align with the buyer’s brand identity and market strategy.
Consider Quality Systems
Food safety and quality management should be considered before starting a long-term manufacturing relationship.
International buyers can review applicable certifications, production procedures, quality-control systems, documentation practices, and product testing requirements when evaluating a supplier.
Assess Communication and Export Support
Effective communication can make a significant difference in international manufacturing projects. Buyers should look for a partner that can clearly communicate specifications, sampling stages, production schedules, packaging requirements, and shipping arrangements.
A manufacturer experienced in export projects can also help international buyers coordinate the different stages required to move from product concept to commercial shipment.
Conclusion
Vietnam offers a combination of agricultural resources, food-processing capabilities, flexible product development, competitive production conditions, and access to international markets that can support the needs of global beverage businesses. Beverage Manufacturing in Vietnam can cover the complete journey from product concept and formula development to commercial production, customized packaging, quality control, and export preparation. For international brands, selecting the right manufacturing partner remains essential to achieving consistent product quality and building a scalable supply chain. Thanh Cong Vina provides customized beverage solutions for companies seeking fruit juice drinks, coconut beverages, aloe vera drinks, RTD coffee, and other beverage concepts for global markets. With an export-oriented approach and integrated manufacturing capabilities, Thanh Cong Vina can support businesses throughout different stages of beverage development. For companies seeking reliable Beverage Manufacturing solutions in Vietnam, the country provides a practical foundation for developing customized products and expanding into international markets.
